Introduction
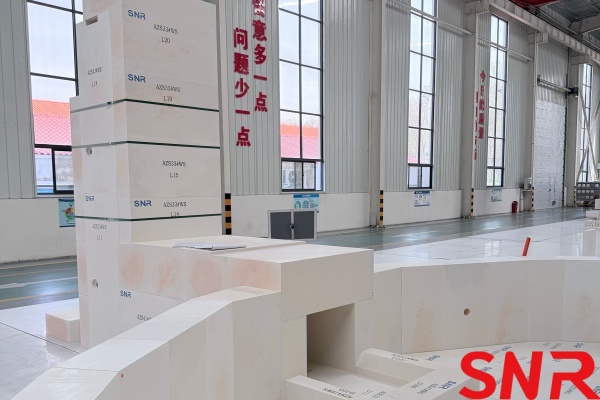
In the glass melting process, the selection of refractory materials directly affects glass furnace lifespan, glass quality, energy consumption levels, and overall operating costs. As the core material for glass furnace linings, AZS (alumina-zirconia-silica) series refractory materials have become indispensable key foundational materials in the modern glass industry, owing to their excellent resistance to glass melt corrosion and high-temperature mechanical strength.
Beyond their intrinsic corrosion resistance, fused cast AZS refractories also play a critical role in maintaining glass melt homogeneity by minimizing the formation of stones (solid inclusions) and cords (streaks of compositional variation). Their chemical inertness toward molten glass reduces the dissolution of refractory components into the melt, which is particularly important for high-clarity applications such as float glass and display substrates. Moreover, the thermal insulation performance of AZS materials, when properly engineered, contributes to reduced heat loss through glass furnace walls, directly impacting specific energy consumption (SEC) metrics—a growing priority under global carbon reduction mandates.
However, faced with the wide variety of AZS products on the market—ranging from fused-cast AZS to sintered AZS, from different zirconia-content grades to various forming processes, along with alternative solutions such as high-alumina bricks and zircon bricks—engineering and technical personnel often find themselves perplexed when making material selections: Is fused-cast AZS or sintered AZS more suitable? Does higher-zirconia AZS necessarily mean superior performance? What are the differences in refractory requirements for different glass categories?
Additional practical challenges include the trade-off between initial capital expenditure and long-term maintenance costs, as well as the availability of specific grades in large block sizes required for modern mega furnaces. The interaction between refractory materials and advanced melting technologies—such as oxy-fuel combustion, electric boosting, and submerged combustion—further complicates the selection landscape. These factors demand a systematic, zone-specific approach rather than a one-size-fits-all philosophy.
This article starts from the fundamentals of materials science, systematically compares the technical characteristics of various refractory materials, and combines the working conditions and failure mechanisms of different zones in glass furnaces to provide readers with a complete selection framework ranging from performance parameters to engineering decision-making. The goal is to help achieve an optimal balance between technical reliability and economic rationality.
1. Fundamentals of AZS Refractories for Glass furnaces
1.1 What is AZS?
AZS is the abbreviation for the Al₂O₃–ZrO₂–SiO₂ ternary refractory system, widely recognized as one of the most important refractory materials used in modern glass furnaces. The three primary components play different roles in the material‘s performance:
► ZrO₂ (Zirconia) significantly enhances resistance to glass corrosion and is the key component determining corrosion resistance.
► SiO₂ (Silica) regulates sintering behavior and thermal expansion characteristics.
Within the ternary phase diagram, the outstanding performance of AZS refractories originates from their eutectic microstructure and the transformation-toughening mechanism of zirconia. When the ZrO₂ content is maintained within the range of approximately 33%–41%, the material achieves an optimal balance between corrosion resistance and thermal shock stability.
The phase relationship in the Al₂O₃–ZrO₂–SiO₂ system is characterized by a eutectic temperature of approximately 1860°C, where corundum (α-Al₂O₃), baddeleyite (monoclinic ZrO₂), and mullite (3Al₂O₃·2SiO₂) coexist in equilibrium. The glassy phase, which occupies the interstitial regions between crystalline phases, serves as a binder but also represents a weak point against chemical attack. During service, the glassy phase can be leached out by molten glass or alkali vapors, leading to structural degradation. Therefore, controlling the composition and distribution of the glassy phase—typically achieved through optimized melting and annealing schedules—is as critical as maximizing crystalline phase content.
1.2 Fundamental Differences in Manufacturing Processes
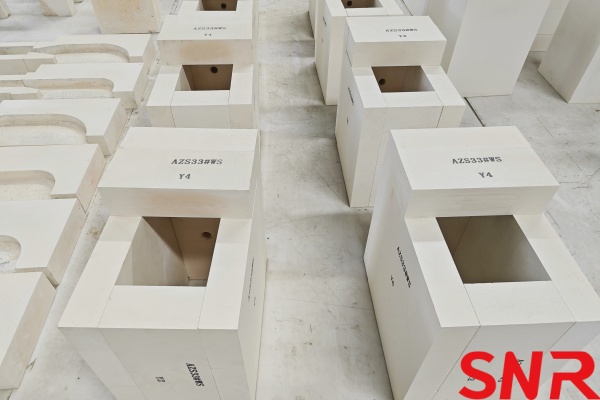
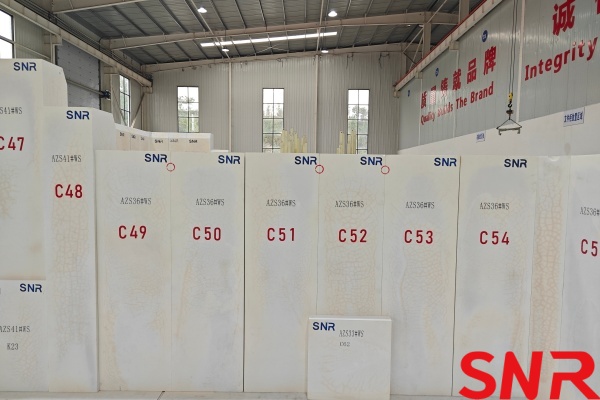
Fused Cast AZS Block
Fused Cast AZS is manufactured by melting the batch materials in an electric arc glass furnace at temperatures exceeding 2000°C. The molten material is then cast into molds and subsequently annealed under controlled cooling conditions to form dense refractory blocks.
Its main characteristics include:
► Coarse-grained microstructure
► Glassy phase content of approximately 15%–25%
► A microstructural gradient from the surface to the interior of the block
The casting process induces a directional solidification pattern, with finer crystals forming near the mold surface due to rapid cooling, while coarser, interlocked eutectic structures develop in the interior. This gradient results in a dense, corrosion-resistant "skin" layer that is particularly beneficial in glass-contact applications. However, the anisotropy of thermal expansion between the surface and core also necessitates careful annealing to prevent cracking during production and subsequent furnace heating schedules.
Sintered AZS
Sintered AZS is produced by finely grinding raw materials, shaping them into bricks, and firing them at high temperatures of approximately 1600–1750°C. Densification is achieved through solid-state diffusion during the sintering process.
Its main characteristics include:
► Fine-grained microstructure
► Lower glassy phase content (approximately 5%–10%)
► Better structural homogeneity
The sintering process allows for tighter dimensional control and greater flexibility in producing complex shapes compared to fused-cast blocks. The finer grain size also contributes to improved thermal shock resistance, as microcracks generated during the monoclinic-to-tetragonal zirconia phase transition (occurring at approximately 1170°C) are better distributed throughout the microstructure, providing crack deflection and energy dissipation pathways.
The fundamental differences between these manufacturing processes determine the distinct positioning of the two materials in terms of corrosion resistance, thermal shock performance, and overall cost-effectiveness.
2. Fused Cast AZS vs. Sintered AZS: Comprehensive Technical Comparison and Material Selection Guide
This chapter serves as the core reference for engineering decision-making. The comparison is conducted from six key perspectives, combining both quantitative and qualitative evaluations.
2.1 Resistance to Glass Corrosion
|
Evaluation Index |
Fused Cast AZS |
Sintered AZS |
|
Corrosion Rate (Relative Value, based on Fused Cast AZS-41 = 1.0) |
1.0 |
1.6–3.0 |
|
Reaction Layer Thickness (1500°C × 168 h) |
0.5–1.5 mm |
2.5–6.0 mm |
|
Tendency to Generate Stones and Cords |
Low |
Medium to High |
The dense structure and coarse eutectic microstructure of fused cast AZS provide superior resistance to glass penetration and dissolution. In particular, when zirconia particles are uniformly distributed within the corundum matrix, they effectively block penetration paths for molten glass. By contrast, the higher open porosity of sintered AZS allows molten glass to infiltrate more easily, accelerating structural degradation.
The corrosion mechanism in AZS refractories involves two simultaneous processes: dissolution of the refractory phases into the glass melt, and penetration of the melt into the refractory microstructure through interconnected pores and grain boundaries. In sintered AZS, the higher porosity provides rapid infiltration pathways, causing accelerated formation of a reaction layer composed of glassy phase enriched with Al₂O₃ and ZrO₂. This layer tends to spall off during thermal cycling, exposing fresh surfaces to further attack. In fused cast AZS, the near-zero porosity effectively suppresses melt infiltration, confining corrosion to a slow, diffusion-controlled dissolution process.
Key Selection Considerations
In highly corrosive zones such as: Doghouse areas, Glass line regions, Throat blocks. The service life of fused cast AZS can be two to three times longer than that of sintered AZS. For large float glass furnaces designed for campaigns exceeding eight years, a fully fused-cast solution has become the industry standard.
2.2 Thermal Shock Resistance
|
Evaluation Index |
Fused Cast AZS |
Sintered AZS |
|
Thermal Expansion Coefficient (20–1000°C, ×10⁻⁶/°C) |
6.5–7.5 |
5.5–6.5 |
|
Thermal Shock Resistance Factor (Relative Value) |
0.3–0.5 |
1.0 |
|
Critical Temperature Difference (ΔT) |
80–150°C |
250–400°C |
Because of its higher porosity and finer grain structure, sintered AZS can absorb thermal stresses more effectively during rapid temperature fluctuations. As a result, its thermal shock resistance is significantly better than that of fused cast AZS.
The superior thermal shock performance of sintered AZS is also attributable to its lower elastic modulus and higher strain tolerance. The presence of microcracks, formed by the volume expansion associated with the zirconia monoclinic-to-tetragonal transformation during cooling from firing temperature, acts as a built-in stress-relief mechanism. This phenomenon, known as microcrack toughening, allows sintered AZS to accommodate thermal gradients without catastrophic failure—a critical advantage in furnace crowns and breast walls that experience rapid temperature swings during batch charging or combustion mode changes.
This explains why sintered AZS is still widely used in areas such as: Glass furnace crowns, Breast walls, other zones subject to frequent temperature fluctuations.
Key Selection Considerations
If the glass furnace experiences: Frequent shutdown and restart cycles, Oxy-fuel combustion operation, Increased thermal gradients. It is advisable to retain sintered AZS in thermal-shock-sensitive areas or select specially toughened formulations.
2.3 High-Temperature Mechanical Strength
|
Evaluation Index |
Fused Cast AZS |
Sintered AZS |
|
Cold Crushing Strength (MPa) |
250–400 |
80–150 |
|
Hot Modulus of Rupture at 1400°C (MPa) |
12–25 |
5–10 |
|
Refractoriness Under Load, T₀.₆ (°C) |
>1700 |
1600–1680 |
|
Creep Rate (1500°C × 50 h, %) |
0.2–0.5 |
1.0–2.5 |
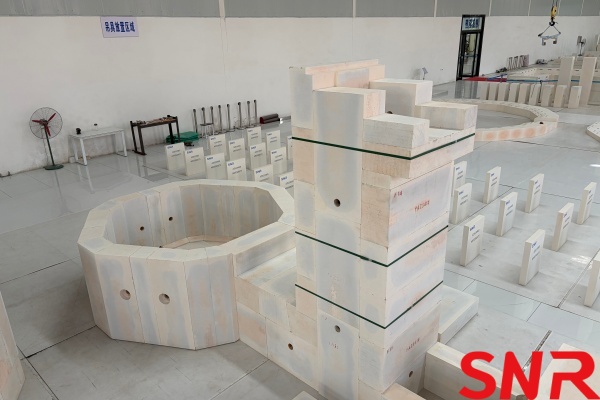
Fused cast AZS demonstrates substantially better structural stability at elevated temperatures. This characteristic is especially important for critical glass furnace components such as: Skew blocks, Suspended wall support blocks, Tongue blocks. Which must withstand structural loads and high-temperature gas flow erosion.
3. AZS vs. High-Alumina Brick vs. Zircon Brick: Application Boundaries and Material Selection Logic
Beyond the AZS family, high-alumina bricks and zircon bricks represent two important alternative classes of refractories that occupy distinct application niches in glass furnace construction. High-alumina bricks (Al₂O₃ content typically 75–99%) offer excellent cost-effectiveness and thermal shock resistance, making them suitable for superstructure and regenerator applications. Zircon bricks (ZrO₂ content > 65%, often stabilized with CaO or MgO) exhibit exceptional resistance to alkali vapor attack and borosilicate corrosion, but their high density and cost restrict them to specialized zones. Understanding the performance boundaries and economic trade-offs among these three material families is essential for rational design optimization.
3.1 Comparative Performance Framework
The selection among AZS, high-alumina, and zircon bricks is governed by four primary performance attributes:
|
Attribute |
AZS (Fused Cast) |
High-Alumina Brick (≥90% Al₂O₃) |
Zircon Brick (≥65% ZrO₂) |
|
Corrosion Resistance to Soda-Lime Glass |
Excellent |
Moderate–Good |
Good |
|
Corrosion Resistance to Borosilicate Glass |
Good–Excellent (high-ZrO₂ grade) |
Poor–Moderate |
Excellent |
|
Thermal Shock Resistance |
Moderate |
Excellent |
Poor |
|
Alkali Vapor Resistance |
Good |
Moderate |
Excellent |
|
Relative Cost (per ton) |
1.0 (baseline) |
0.4–0.6 |
2.0–3.5 |
3.2 Application Boundary Guidelines
High-Alumina Bricks are recommended for:
► Regenerator checkerwork upper courses (where alkali condensation is less severe)
► Forehearth superstructures and distributor channel covers
► Temporary repair patches and backup linings
Zircon Bricks are recommended for:
► Glass contact zones in opal glass (fluorine-containing) and high-PbO glass furnaces
► Sidewalls of electric melting furnaces where aggressive alkali species are present
► Critical ports in oxy-fuel furnaces where alkali sulfate condensation is severe
4. AZS Series Grade Classification and Performance Characterization
Within the AZS family itself, however, not all grades are created equal. The zirconia content, microstructure, and glassy phase composition vary significantly among commercial products, leading to distinct performance attributes. The following chapter provides a systematic classification of AZS grades and establishes the scientific basis for grade selection.
4.1 Standard Grade Classification
Currently, AZS refractories are classified into three standard grades based on ZrO₂ content:
|
Grade |
ZrO₂ Content (wt%) |
Typical Al₂O₃ Content (wt%) |
Typical SiO₂ Content (wt%) |
|
AZS-33 |
32–34% |
48–52% |
14–16% |
|
AZS-36 |
35–37% |
46–50% |
12–14% |
|
AZS-41 |
40–43% |
44–48% |
10–12% |
The glassy phase in AZS refractories is not merely a residual binder but a carefully engineered component that influences densification, thermal expansion, and exudation behavior. Its composition typically lies within the Na₂O–Al₂O₃–SiO₂ system, with Na₂O content ranging from 1.5% to 3.0%. Higher Na₂O levels reduce the glassy phase viscosity at elevated temperatures, promoting densification during casting but also increasing the risk of exudation during furnace operation. Exuded glassy phase can react with molten glass to form cords or dissolve into the melt, affecting product quality. Therefore, premium-grade AZS products feature precisely controlled glassy phase compositions with low Na₂O (< 2.0%) and high Al₂O₃/SiO₂ ratios to minimize exudation at typical glass melting temperatures of 1500–1600°C.
4.2 Microstructure Characteristics of Different Grades
The grade-dependent performance of AZS refractories is rooted in their microstructural evolution during solidification. As ZrO₂ content increases from 33% to 41%, the volume fraction of the eutectic (corundum + baddeleyite) phase increases, while the primary corundum phase decreases. In AZS-33, the microstructure is dominated by large corundum dendrites embedded in a fine eutectic matrix. In AZS-41, the eutectic structure becomes more continuous and interlocking, providing superior resistance to glass penetration. However, the higher ZrO₂ content also increases the amount of monoclinic phase retained at room temperature, contributing to higher thermal expansion and reduced thermal shock resistance.
4.3 Scientific Basis for AZS Grade Selection
The contribution of zirconia content to corrosion resistance follows a clear threshold effect rather than a linear relationship.
Improvement in Corrosion Resistance
When the ZrO₂ content increases:
► From 36% to 41%, the improvement is only about 5–10%.
This demonstrates a typical law of diminishing marginal returns. In other words, increasing zirconia content beyond a certain level yields progressively smaller gains in corrosion resistance.
Trade-Offs Associated with Higher Zirconia Content
Increasing ZrO₂ content also brings several disadvantages:
► Reduced thermal shock resistance
► Higher glassy-phase exudation temperature, which may increase the risk of bubble formation during initial glass furnace operation
► Significantly increased material cost
► Greater machining and cutting difficulty
Therefore, AZS grade selection should not be based solely on maximizing zirconia content. Instead, it should balance corrosion resistance, thermal stability, glass furnace design requirements, and project economics.
4.4 Grade Selection Recommendations
Typical Applications for AZS-33
► Tableware glass furnaces
► Forehearths and distributor channels
► Regenerator partition walls operating below 1500°C
► Superstructures of small and medium-sized glass furnaces
► Intermittently operated glass furnaces where cost control is important
AZS-33 provides the most economical solution while maintaining acceptable corrosion resistance.
Typical Applications for AZS-36
► Melting zones of photovoltaic rolled-glass furnaces
► Large container glass furnaces
► Cost-effective alternatives to AZS-41
AZS-36 is often considered the "workhorse grade" of modern glass furnaces because it provides an excellent balance between performance and cost.
Typical Applications for AZS-41
► Glass line areas in photovoltaic glass furnaces
► Throats
► Doghouses
► Sidewalls exposed to highly corrosive glasses such as borosilicate glass and opal glass
► Long-campaign glass furnaces designed for service lives exceeding eight years
► Areas surrounding electric boosting electrodes
These applications demand maximum resistance to glass corrosion and erosion.
5. Is High-Zirconia AZS Always Better? — The Art of Balancing Cost and Performance
5.1 Reassessing the Advantages of High-Zirconia AZS
In recent years, some manufacturers have introduced so-called High-Zirconia AZS products containing more than 45% or even 50% ZrO₂, promoting them as offering "superior corrosion resistance." Laboratory static crucible corrosion tests indeed show that High-Zirconia AZS (approximately 50% ZrO₂) can reduce corrosion rates by approximately 20–30% compared with conventional AZS-41. However, this laboratory advantage often does not translate proportionally into actual glass furnace campaign life.
The reasons are discussed below.
Reason 1: Multiple Failure Mechanisms Govern Refractory Life
Sidewall refractory failure is rarely determined by corrosion resistance alone. The actual service life is influenced by multiple factors, including:
► Mechanical erosion
► Thermal shock
► Structural stress
► Glassy-phase exudation
► Operational conditions
In one industrial case, High-Zirconia AZS experienced less corrosion but suffered premature structural cracking caused by thermal-expansion mismatch, ultimately shortening the glass furnace campaign.
Reason 2: Hidden Risks to Glass Quality
High-Zirconia AZS requires special adjustment of the glassy-phase composition. If process control is inadequate:
► Fine zirconia particles may enter the glass melt.
► Zircon stones may form in the final product.
For high-quality glass production, this risk can outweigh the potential gains in corrosion resistance.
Reason 3: Increased Manufacturing Complexity
When zirconia content exceeds approximately 45%, the fused-casting process becomes substantially more difficult. The likelihood of manufacturing defects increases, including:
► Shrinkage cavities
► Internal cracks
► Structural heterogeneity
As a result, product consistency and reliability become more difficult to maintain.
5.2 Quantitative Cost-Benefit Analysis
The following comparison uses glass-line sidewall applications as an example.
|
Option |
Relative Material Cost |
Expected Service Life |
Annualized Cost |
Risk Adjustment Factor |
|
AZS-36 |
1.00 |
6 Years |
0.167 |
1.0 |
|
AZS-41 |
1.65 |
9 Years |
0.183 |
0.9 |
|
High-Zirconia AZS (~50% ZrO₂) |
2.80 |
10 Years |
0.280 |
1.5 |
The risk adjustment factor reflects uncertainties associated with:
► Glass quality fluctuations
► Installation complexity
► Manufacturing consistency
The analysis shows that:
► Service life increases by only about 11%.
► The overall cost-performance ratio is significantly lower.
5.3 Application Recommendations
High-Zirconia AZS should be considered only for extremely demanding applications, such as:
High-Borosilicate Glass furnaces
Applications where:
► Severe chemical corrosion occurs
Electromagnetic Stirring Zones
Areas characterized by:
► Extremely aggressive flow conditions
Premium Specialty Glass Production
Examples include:
► TFT-LCD substrate glass
► High-performance electronic glass
For more than 95% of glass furnace applications, AZS-41 already represents the optimal balance between: Corrosion resistance, Glass furnace campaign life, Glass quality, Investment cost. Blindly pursuing higher zirconia content is neither technically justified nor economically efficient. In refractory engineering, the best material is not necessarily the most expensive one, but the one that best matches the operating conditions of the glass furnace.
6. AZS Refractory Selection for Different Glass Types
Due to differences in chemical composition, melting temperature, viscosity characteristics, and product quality requirements, different glass categories impose distinct demands on AZS refractory selection.
6.1 Float Glass
Process Characteristics
► Glass composition: Soda-lime-silica system (SiO₂ ≈ 72%, Na₂O ≈ 14%, CaO ≈ 9%)
► Viscosity: Relatively low at high temperature, good flowability
► Quality requirements: Extremely high (optical distortion < 0.1%)
► Glass furnace campaign life: 8–12 years
Influence on Refractories
► Tin bath reducing atmosphere is highly sensitive to iron contamination (Fe₂O₃ < 0.5% is a critical threshold).
► Strong convection currents increase glass line corrosion severity.
Recommended AZS Selection
|
Glass furnace Area |
Recommended Grade |
Iron Content Requirement |
Key Performance Requirement |
|
Sidewall Glass Line |
AZS-41 |
Fe₂O₃ < 0.5% |
High corrosion resistance, low glass phase exudation |
|
Sidewall Lower Zone |
AZS-36 |
Fe₂O₃ < 0.8% |
Corrosion resistance |
|
Throat |
AZS-41 |
Fe₂O₃ < 0.5% |
High density, low porosity |
|
Crown |
Sintered AZS-36 |
Fe₂O₃ < 1.0% |
Alkali resistance, thermal shock resistance |
|
Doghouse |
AZS-41 |
Fe₂O₃ < 0.5% |
Thermal shock + corrosion resistance |
Engineering Example
A high-end float glass line with a daily output of 1000 tons uses imported AZS-41 (ZrO₂ ≈ 41.5%) at the glass line region, combined with forced air cooling. After 9 years of operation:
► Expected glass furnace campaign life: ~12 years
6.2 Photovoltaic (Solar) Glass — Rolled Process
Process Characteristics
► Glass composition: Soda-lime-silica with minor flux additives
► Viscosity: Higher than float glass
► Iron content: Extremely low (Fe₂O₃ < 0.015%)
► Quality requirements: Transmittance > 91.5%, strict control of bubbles and stones
► Glass furnace campaign life: 7–10 years
Influence on Refractories
► Higher melting temperature significantly increases corrosion rate.► Ultra-low iron glass is extremely sensitive to refractory contamination (Fe₂O₃ > 0.6% may cause discoloration).
► Requires highly uniform melt quality for rolling process stability.
Recommended AZS Selection
|
Glass furnace Area |
Recommended Grade |
Special Requirement |
|
Sidewall (Entire Tank) |
AZS-41 |
Fe₂O₃ < 0.4%, low glass phase exudation |
|
Throat |
AZS-41 |
High density, Fe₂O₃ < 0.4% |
|
Crown |
Fused Cast AZS-36 or High-Purity Sintered AZS |
Alkali resistance, low volatile components |
|
Doghouse |
AZS-41 |
Enhanced thermal shock resistance |
6.3 Container Glass (Bottles & Tableware)
Process Characteristics
► Composition: Soda-lime-silica system, sometimes with PbO or BaO additions
► Production mode: Multi-product, small batch, frequent changeover
► Quality requirements: Moderate (higher tolerance for bubbles and cords)
► Glass furnace type: Regenerative end-fired glass furnaces
► Campaign life: 5–8 years
Influence on Refractories
► Color glass production may contain heavy metal oxides (Cr₂O₃, CoO), increasing chemical attack.
► High sensitivity to cost due to market competition.
Recommended AZS Selection
|
Furnace Area |
Recommended Grade |
Cost-Optimized Alternative |
|
Sidewall |
AZS-33 (small furnaces) / AZS-36 (large furnaces) |
High-quality sintered AZS |
|
Throat |
AZS-36 |
AZS-33 (small furnaces) |
|
Crown |
Sintered AZS-33 |
High-alumina brick (<1500°C) |
|
Doghouse |
AZS-36 |
AZS-33 |
Special Notes
► Opal glass (fluorine-containing) is highly aggressive; high-zirconia AZS or enhanced cooling is often required.
► Frequent color change glass furnaces may benefit from fused cast α-β alumina in forehearths to reduce contamination.
6.4 Specialty Glass (Borosilicate, Glass Ceramics, etc.)
Process Characteristics
► Strong chemical attack from B₂O₃
► Glass ceramics contain TiO₂ and ZrO₂ nucleating agents, increasing chemical complexity
► Extremely strict product quality requirements (pharmaceutical, heat-resistant glass)
Influence on Refractories
► Complex interaction between glass chemistry and refractory phases.
► Very limited tolerance for contamination defects.
Recommended AZS Selection
|
Furnace Area |
Recommended Solution |
|
Sidewall (Glass Contact) |
High-Zirconia AZS (ZrO₂ ≥ 45%) or special boron-resistant formulations |
|
Critical Zones |
Zircon Brick or fused cast alumina may be preferable in specific cases |
Engineering Recommendation
Special glass applications require:
► Laboratory corrosion testing
► Close cooperation between glass technologists and refractory suppliers
Standard AZS grades may not always be sufficient.
7. Integrated Selection Decision Framework
7.1 Five-Step Selection Process
A systematic refractory selection process for glass furnaces should follow a structured engineering methodology rather than empirical judgment alone.
Step 1: Define Operating Conditions
The first step is to clearly define all key process parameters:
Melting temperature and temperature uniformity requirements
Furnace design campaign life
Production capacity (daily melting tonnage)
Fuel type and combustion method
These parameters determine the overall thermal and chemical load on refractories.
Step 2: Identify Failure Mechanisms by Furnace Zone
A detailed furnace cross-section should be established to analyze:
Temperature distribution profileGas flow patterns
Glass flow behavior
For each furnace zone, the dominant failure mechanisms must be identified:
Mechanical erosion
Thermal shock
Alkali vapor attack
Structural stress
This step ensures that material selection is based on actual service conditions rather than generic assumptions.
Step 3: Preliminary Material Screening
Based on the application boundaries defined in previous chapters, candidate materials are selected for each zone.
Typically, 2–3 alternative materials should be identified per location, such as:
Sintered AZS
High-alumina bricks
Zircon bricks
α-β alumina blocks
This creates a realistic selection pool for further evaluation.
Step 4: Technical and Economic Evaluation
Each candidate solution must be evaluated using a life-cycle cost (LCC) approach, including:
Transportation cost
Installation and construction cost
Furnace downtime loss
Maintenance and repair cost
Product quality risk cost
In modern furnace engineering, material price alone is no longer a reliable decision criterion.
Step 5: Supplier Qualification and Sample Testing
Before final selection, suppliers must be evaluated in terms of:
Quality management system (ISO-based or equivalent)
Consistency of production batches
Technical documentation should include:
Phase composition verification
Apparent porosity and bulk density
Third-party inspection reports
Where necessary, comparative corrosion testing under simulated glass conditions should be conducted to validate performance.
7.2 Quick Selection Decision Matrix
|
Furnace Type |
Target Campaign Life |
Sidewall Recommendation |
Crown Recommendation |
Throat Recommendation |
Optimization Strategy |
|
Large Float Line |
≥10 years |
AZS-41 (glass line) / AZS-36 |
Sintered AZS-36 |
AZS-41 |
Use AZS-41 only in critical zones |
|
Medium Float Line |
8–10 years |
AZS-36 (glass line AZS-41) |
Sintered AZS-33 |
AZS-41 |
Cost optimization in superstructure |
|
Photovoltaic Glass |
≥8 years |
AZS-41 (full tank sidewall) |
Fused Cast AZS-36 |
AZS-41 |
Strict iron control requirement |
|
Large Container Glass |
6–8 years |
AZS-36 (glass line) / AZS-33 |
Sintered AZS-33 |
AZS-36 |
Balance cost and thermal shock |
|
Medium/Small Container Glass |
4–6 years |
AZS-33 |
High-alumina brick |
AZS-33 |
Cost-driven design |
|
Borosilicate Glass |
5–8 years |
High-Zirconia AZS or Zircon Brick |
Fused Cast AZS-41 |
High-Zirconia AZS |
Custom engineering required |
|
Glass Fiber (E-glass) |
6–8 years |
AZS-36 |
Sintered AZS-33 |
AZS-41 |
Fluorine-resistant formulations |
|
Glass Fiber (C-glass) |
5–7 years |
AZS-41 |
Sintered AZS-33 |
Zircon Brick |
High erosion resistance |
Final Conclusion
The selection of AZS refractories is essentially a system engineering optimization problem, balancing:
► Corrosion resistance
► Glass quality requirements
► Service life expectations
► Total lifecycle cost
The key conclusions can be summarized as follows:
Fused Cast AZS and Sintered AZS are complementary, not competing materials
· Fused cast AZS is used in glass-contact, high-corrosion "hot face" zones
· Sintered AZS is used in upper structures and thermal shock zones
Clear application boundaries exist among AZS, high-alumina, and zircon materials
· AZS: Main structural material for glass contact zones
· High-alumina: Cost-effective solution for upper and auxiliary zones
· Zircon: Specialized use under extreme corrosion conditions
Higher zirconia content does not always mean better performance
· Beyond ~41% ZrO₂, performance improvement becomes marginal
· Cost and risk increase significantly
· AZS-41 remains the optimal balance point for most applications
Glass type determines selection priorities
· Float glass: iron control + corrosion resistance
· Photovoltaic glass: ultra-low iron + high temperature resistance
· Container glass: thermal shock resistance + cost efficiency
· Specialty glass: customized chemical resistance
Life-cycle cost is the ultimate decision criterion
Material price represents only a small portion of total furnace cost. Factors such as:
· Furnace downtime
· Glass quality defects
· Maintenance cycles
often have a much greater economic impact.
 I am Zoe. If you have any purchasing plans for fused cast AZS refractory blocks, please contact me.
[email protected]/ WhatsApp:+86 15670323812

 +86-18203976036
